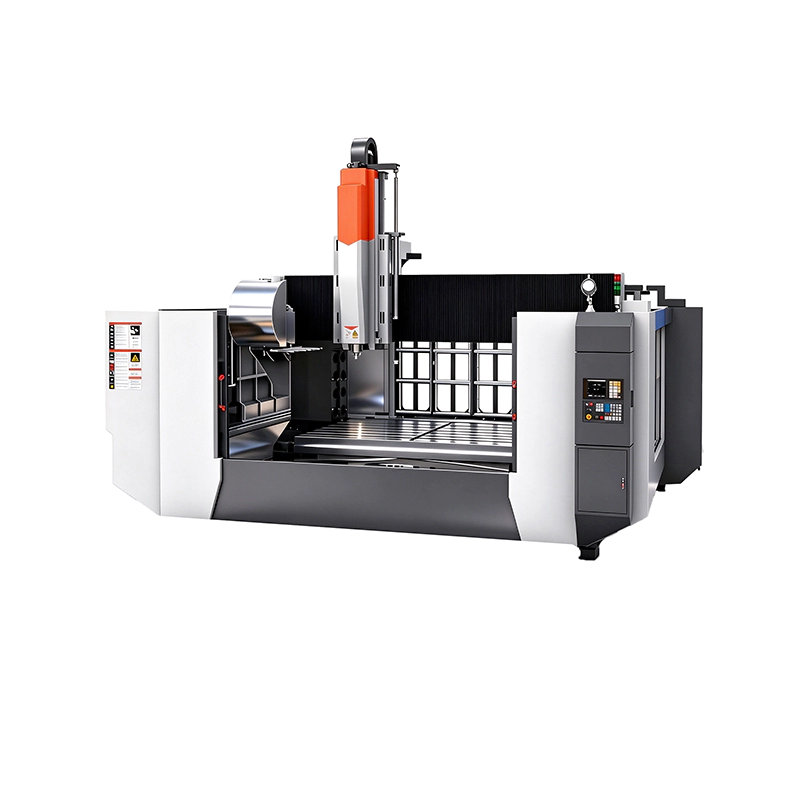
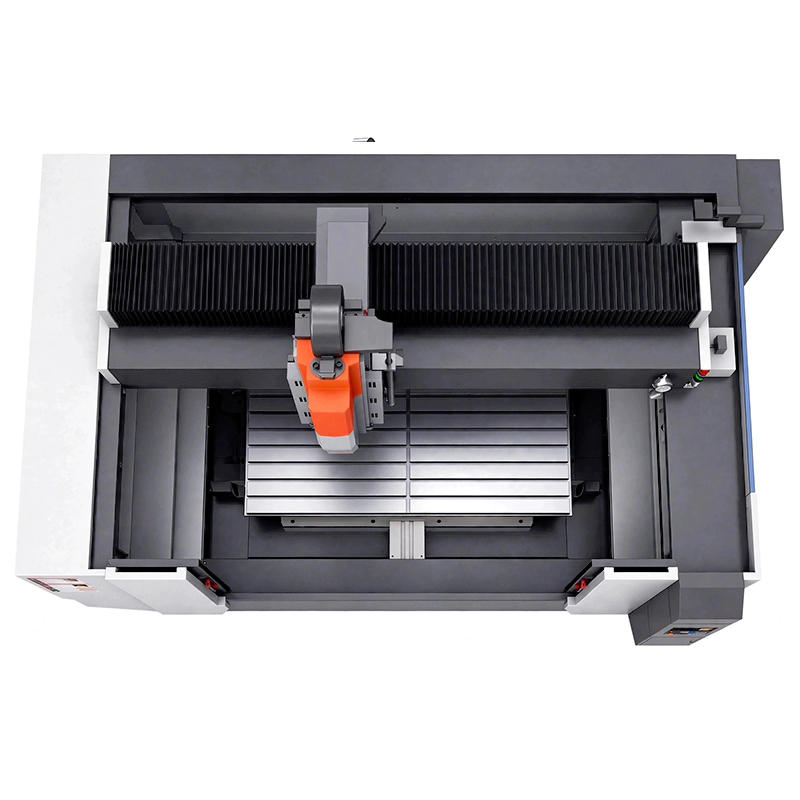
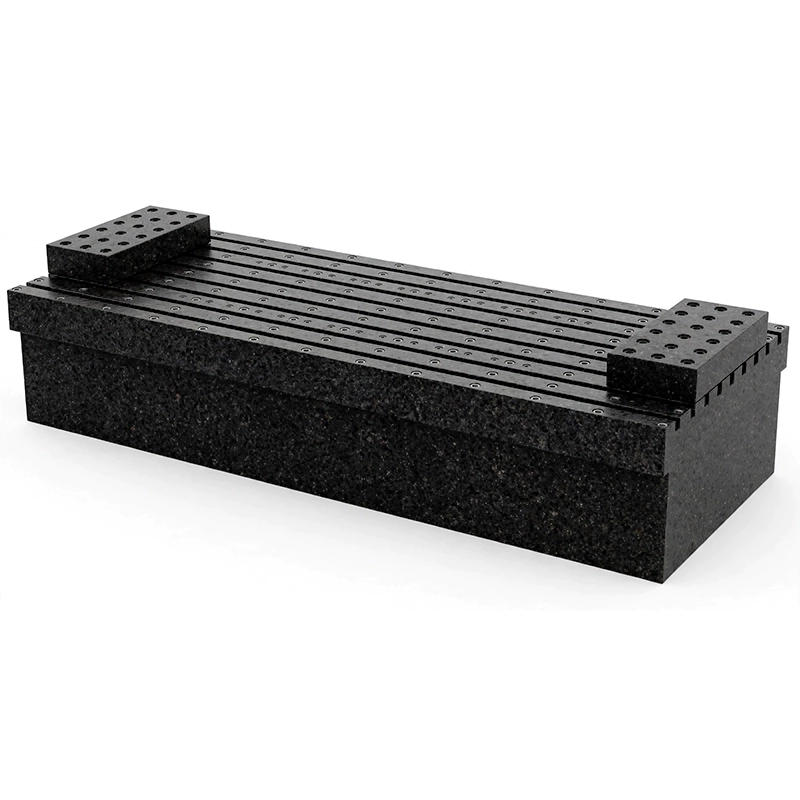
The GMC2013’s base — a single mineral casting of ≈ 12 tonnes — integrates the work-table foundation, coolant and chip channels, anchor system and leveling elements in one pour. The gantry crossbeam is likewise a mineral casting structure with cast-in steel guideway inserts, ground after curing. No weld seams, no bolted frame joints, no thermal stress from a foundry: the structure is stress-free from the day it is cast.
At this scale the material advantages compound: damping up to 10× cast iron suppresses the low-frequency gantry modes that limit heavy cuts; thermal conductivity of ≈ 1/20 of cast iron means a 2-metre structure that barely breathes with the shop’s day-night cycle.
Gantry machines are only as stiff as their worst position — so the GMC2013 was analysed with the spindle head at mid-span and full Z extension, the weakest configuration in the envelope.
| Load case (worst position) | Tool-point displacement (FEM) |
|---|---|
| 3,000 N in X (side milling) | 0.021 mm |
| 3,000 N in Y (face milling) | 0.017 mm |
| 3,000 N in Z (plunge / drilling thrust) | 0.011 mm |
| Table sag under 3,000 kg centred load | 0.009 mm |
| Mode | Natural frequency | Mode shape |
|---|---|---|
| 1st | 48 Hz | Gantry sway in X |
| 2nd | 57 Hz | Crossbeam bending |
| 3rd | 71 Hz | Gantry torsion |
| 4th | 89 Hz | Column / saddle local mode |
Dual-drive synchronisation control plus the frame’s high material damping keep the first gantry mode from being excited in normal roughing and finishing envelopes.
With a 1 K vertical temperature gradient across the structure, simulated tool-point drift is ≤ 0.008 mm; over a ±3 K daily ambient cycle, ≤ 0.012 mm — before any software compensation. Linear-scale feedback closes the remaining growth out of the position loop entirely.
Conclusion: FEM verification at the worst position in the envelope confirms the GMC2013’s structure is never the limiting factor — not in heavy roughing, not in long finishing passes.

| Parameter | GMC2013 |
|---|---|
| Travel X / Y / Z | 2,000 / 1,300 / 600 mm |
| Work table | 2,100 × 1,200 mm, T-slots, max. load 3,000 kg |
| Structure | Mineral casting monolithic base (≈ 12 t) + mineral casting crossbeam, cast-in steel inserts |
| Gantry drive | Dual synchronised AC servo, C5 ball screws (linear-motor X optional) |
| Feedback | Fagor linear scales, all axes |
| Rapid traverse / cutting feed | 20 m/min / up to 10 m/min |
| Positioning accuracy | ±0.010 mm full travel (±0.006 mm with error mapping) |
| Repeatability | ±0.005 mm |
| Spindle | BT50, 15 kW, 6,000 rpm (optional 12,000 rpm) |
| Tool magazine | 24 tools (optional 40) |
| Controller | Fagor 8065 / Siemens 828D (customer choice) |
| Machine weight | ≈ 18,500 kg |
| Applications | Mould & die, aerospace structures, EV battery trays, large plates, rail and energy components |
Share your application, drawing or dimensional requirements with our team.